 Kanger Glass-ceramic Co., Ltd.
Flatness tolerance must be tied to the part size, measurement reference, support condition, temperature, surface, and functional need. State whether the requirement covers overall bow, local waviness, edge lift, or fit to a fixture. Without that definition, two inspectors can obtain different results from the same ceramic-glass panel. For black ceramic glass, the design must also account for cooktop, heater, control-panel, and heat-shield applications where a dark appearance must coexist with controlled thermal behavior. Treat the glass, decoration, seals, frame, and process history as one system rather than selecting the panel from a material name alone.
Define the form error that matters
The phrase black ceramic glass flatness tolerance describes a specific engineering task, not an off-the-shelf material grade. Start by fixing the application, part position, normal and abnormal duty, geometry, neighboring materials, and acceptance evidence. Kanger can review a controlled drawing and application brief, but the equipment maker remains responsible for validating the finished assembly and its safety requirements.
Because the surface is dark and reflective, inspection lighting, viewing angle, print contrast, fingerprints, haze, and edge exposure can change what an inspector sees. That is why the inspection and validation plan should reproduce the way the finished product is built, heated, cleaned, viewed, and handled. A coupon can answer a narrow material question, but it cannot prove the behavior of an unsupported edge, compressed seal, curved frame, printed zone, or full-size panel.
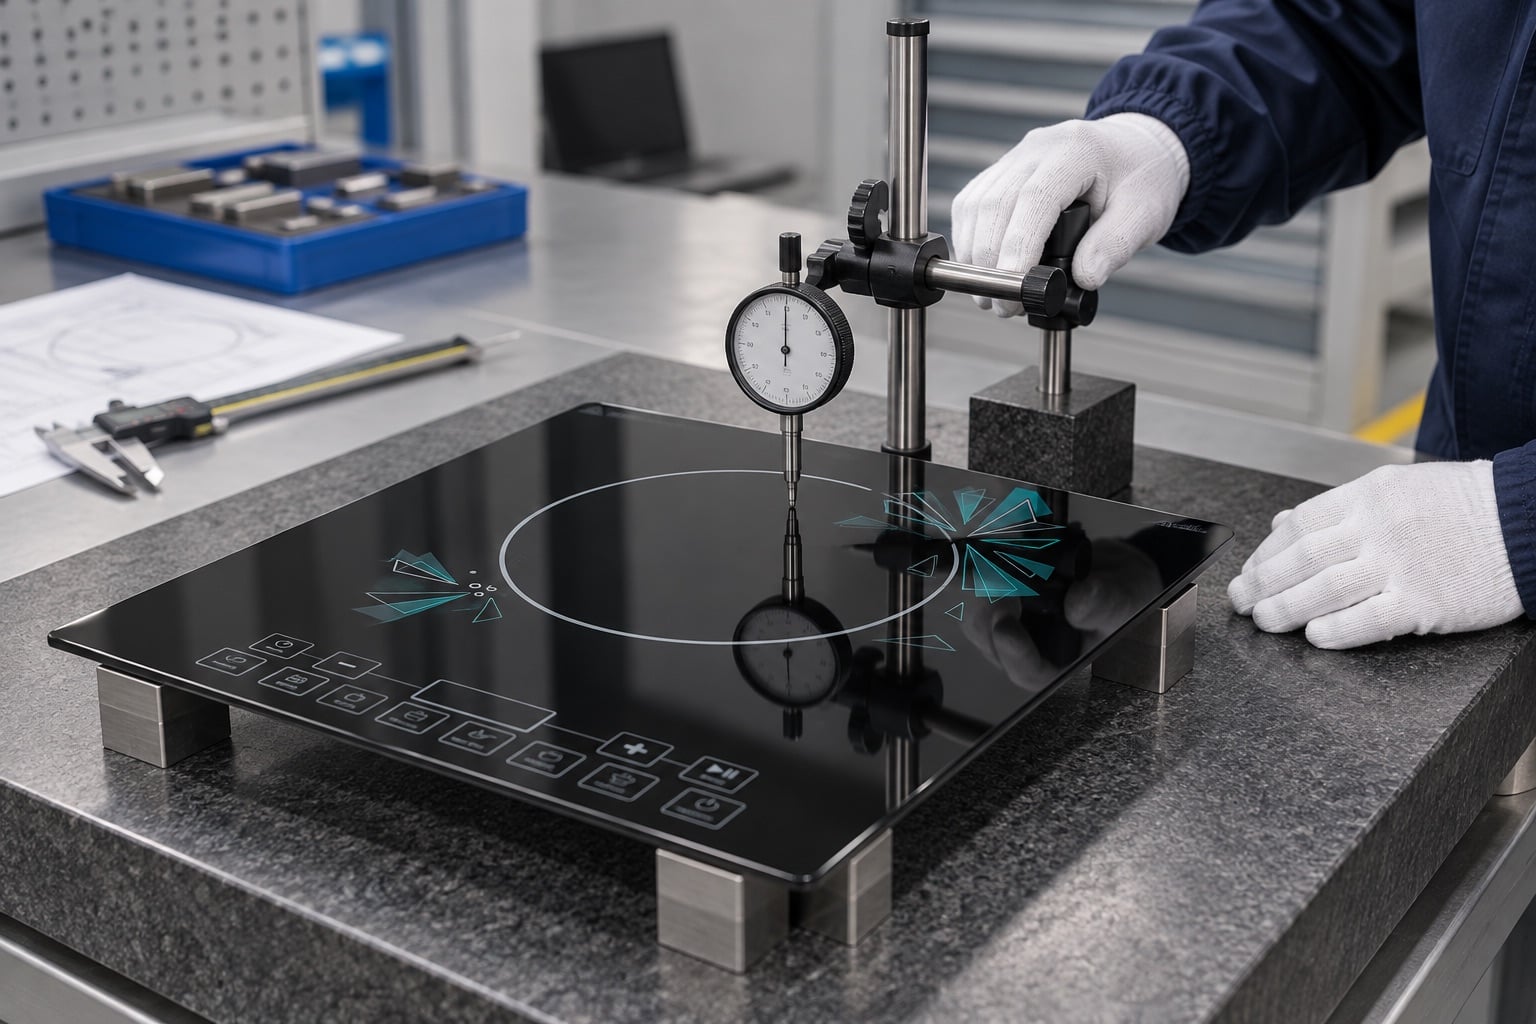
Choose a stable measurement setup
Before requesting quotations, separate confirmed requirements from open questions. Confirmed requirements belong on the drawing or purchase specification. Open questions belong in a deviation list with an owner and due date. This prevents a supplier from filling gaps with assumptions that later become expensive tooling, packing, or assembly changes.
Place the finished part on the agreed support or measurement fixture after it has stabilized at the reference condition. Identify the datum or best-fit method, measurement grid, excluded edge zone, instrument, and reporting resolution. Do not mix free-state and clamped measurements. The result should be understandable by design, sourcing, production, and incoming inspection teams. If the measurement or test cannot be repeated by another qualified person, the requirement is not yet ready for serial production.
For this black ceramic glass programme, list the part function, heat sources, cold boundaries, loads, fluids, cleaners, expected cycles, viewing conditions, installation sequence, and maintenance access. State which values are measured, which are calculated, and which remain provisional. The specification should not turn an unknown condition into an unsupported fixed limit.
Separate overall bow from local distortion
A soft surface, uneven table, debris, protective film, gravity orientation, temperature difference, or clamp force can dominate the reading. A small panel and a large panel should not inherit the same unexplained limit, and a visual reflection issue is not automatically the same as mechanical flatness. Review foreseeable tolerance combinations rather than only nominal CAD geometry. The most important condition is often at a corner, hole, clip, gasket joint, printed border, or transition where temperature and stress are not uniform.
Store the measurement map, maximum and minimum points, instrument ID, setup photo, part orientation, temperature, and heat-process lot. Confirm that the allowed form still supports sealing, printing alignment, sensor coupling, and frame clearance. Link the records to the part number, drawing revision, supplier, material or process lot, and test date. This traceability helps distinguish a one-off handling event from a systematic design or process problem.
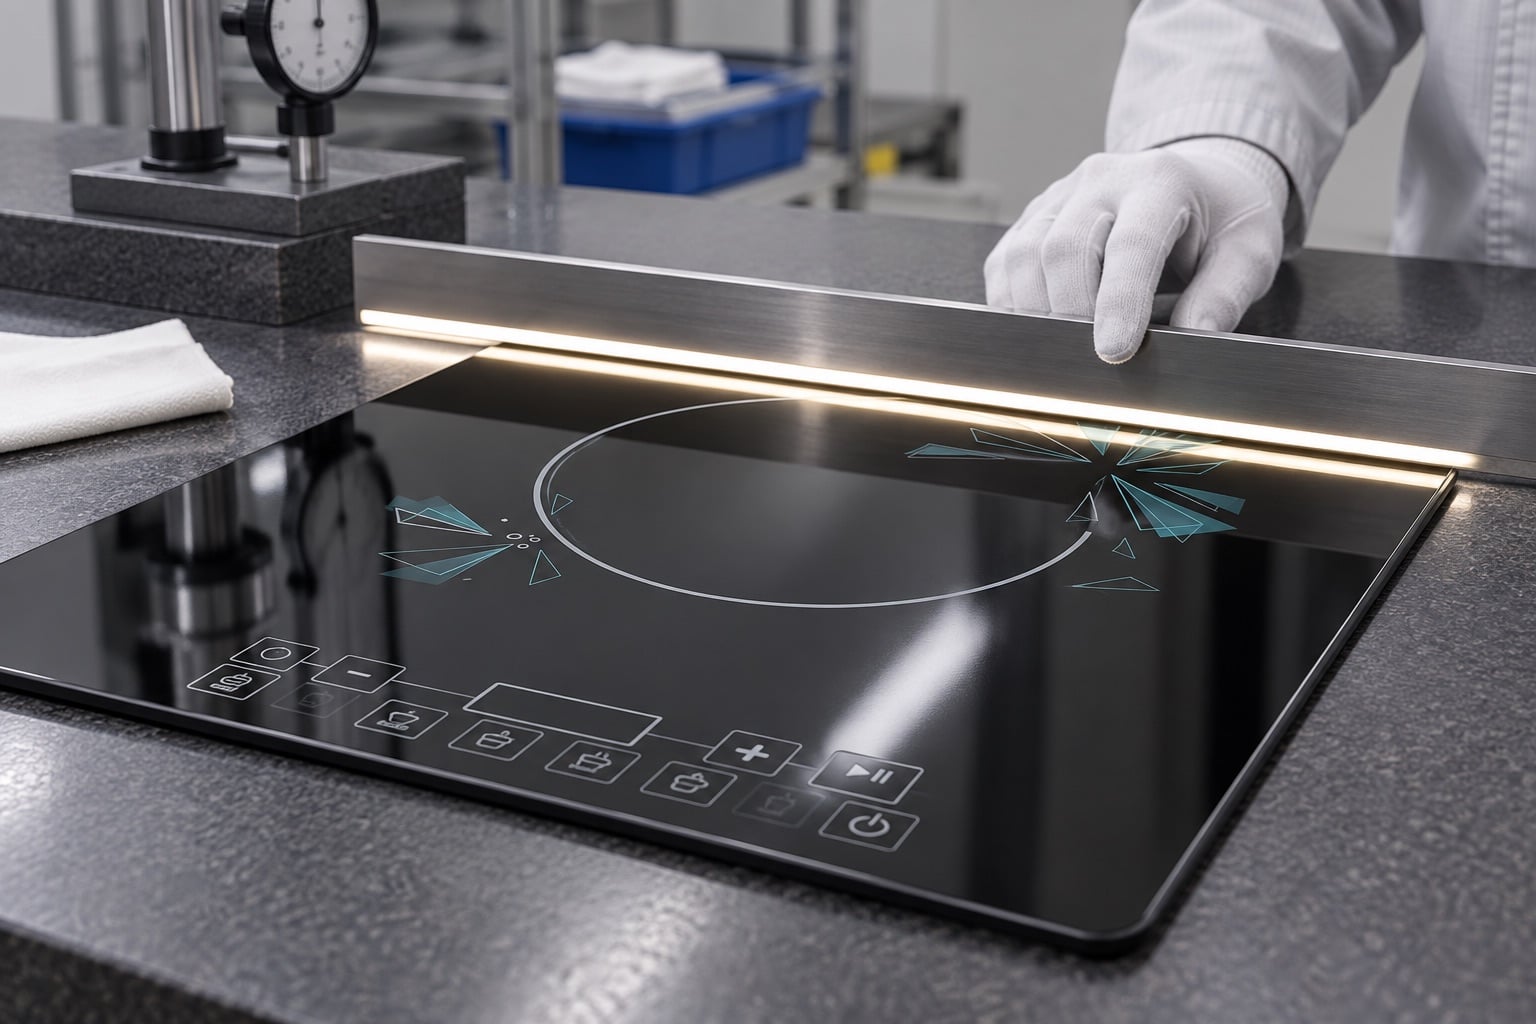
Use the same units, reference temperature, datum system, and orientation throughout the drawing, inspection sheet, test report, and supplier quotation. When a standard method is referenced, identify the edition and any project-specific departures. Where no suitable standard directly applies, write a project method with enough detail for independent repetition.
Connect flatness to assembly function
During supplier review, ask what process creates each controlled feature and what data are produced automatically. A capability statement should name the measured characteristic, method, sample basis, and production period. A general claim such as “high quality,” “heat resistant,” or “within standard” is not a substitute for the buyer’s stated acceptance rule.
First articles should be assembled with production-intent hardware, seals, supports, and cleaning materials. Inspect them before assembly, after assembly, after the representative duty cycle, and after disassembly where practical. Record any witness marks, edge contact, print change, haze, leakage, noise, or fit shift. Do not force a part to pass by modifying the fixture without recording the change.
A production control plan should distinguish checks performed on every part, checks sampled by lot, and periodic qualification tests. Identity, critical cracks, wrong orientation, and missing operations may require different controls from minor appearance variation. The sampling plan must reflect consequence and process stability, not simply the cost of inspection.
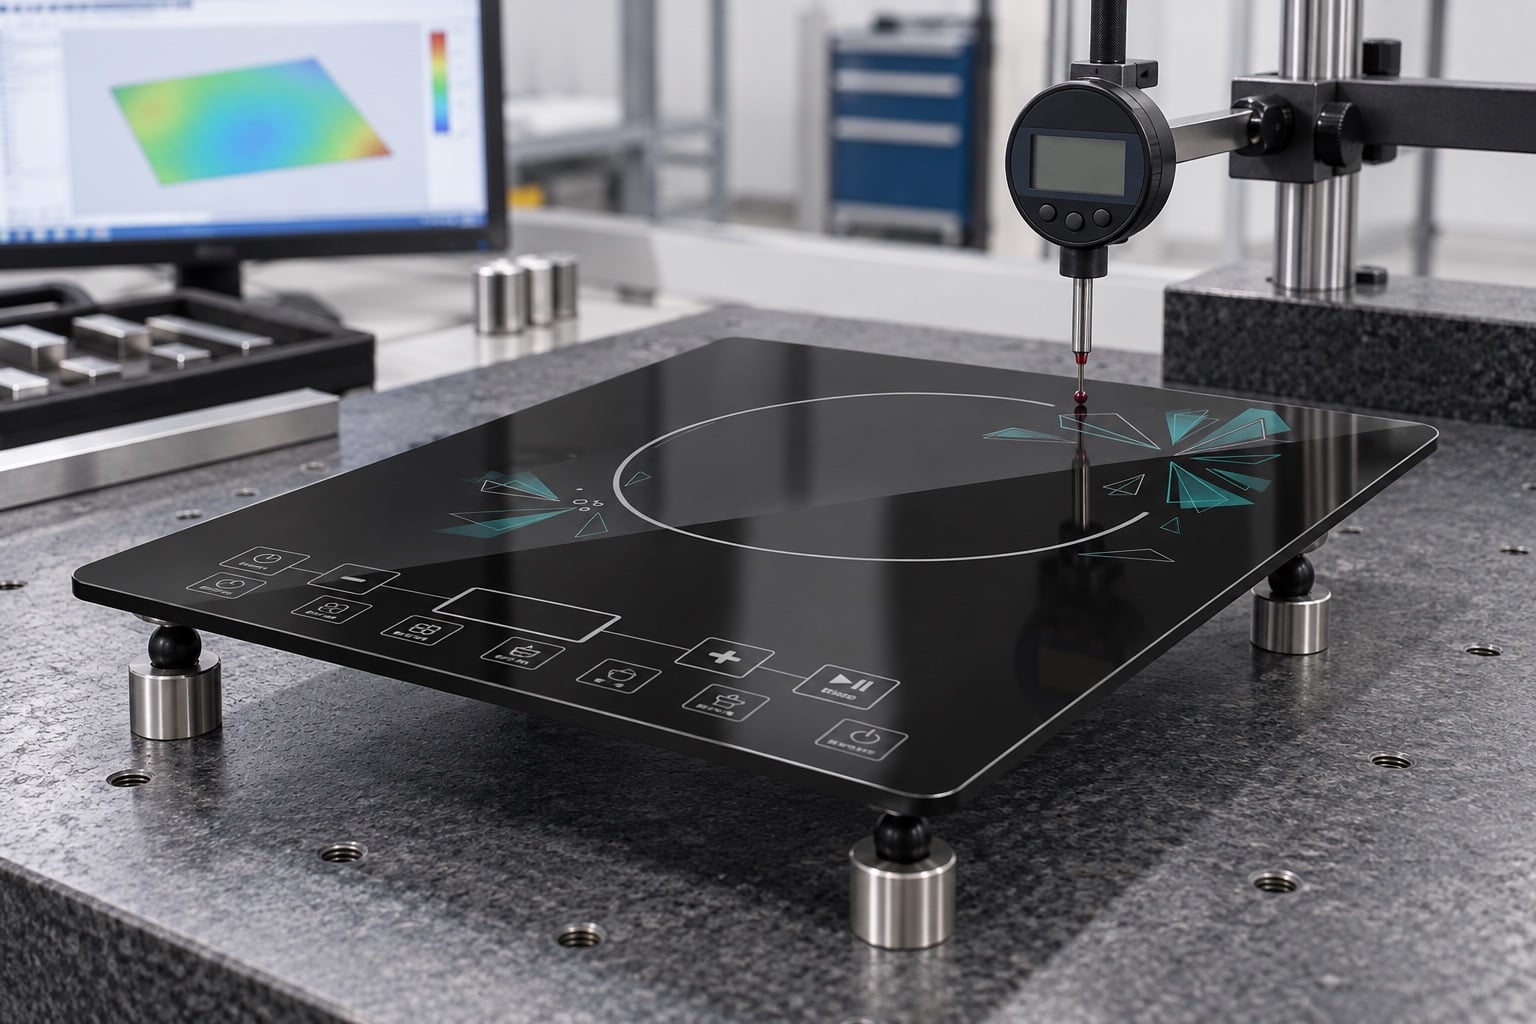
Decision and inspection table
| Control point | What to record | Decision purpose |
|---|---|---|
| Characteristic | Overall bow, local waviness, or edge lift | Name the actual form error |
| Condition | Free state or controlled fixture | Avoid measurement-induced distortion |
| Reference | Datum plane or best fit | Makes results comparable |
| Sampling | Grid and excluded edge zone | Captures local conditions |
| Function | Fit, seal, optics, or bonding | Justifies the tolerance |
Use this table as a planning aid, then replace general wording with project-specific requirements. Do not copy a limit from another product merely because the material family looks similar. The accepted value must suit the size, fabrication route, assembly, operating cycle, and consequence of failure for the actual component.
Control heat-process variation
When a nonconformance appears, contain the affected lot, preserve representative parts, compare the released requirement with the actual inspection method, and determine whether the issue is design, material, process, handling, or documentation. A concession should be explicit, limited, approved, and traceable; it should never silently become the new standard.
Packaging and transport can alter the condition that the factory approved. Use clean separators, edge protection, controlled stacking, compatible film, moisture protection where needed, and carton limits based on trial evidence. Inspect samples from different positions in the pack so edge rub, particle imprint, coating transfer, and bending are not missed.
Change control should cover material source, thickness, cutting route, edge process, heat treatment or ceramization, printing, coating, cleaning, gasket, frame, tool, fixture, software, and packaging. The change notice should state which earlier evidence remains valid and which tests or samples must be repeated before the new condition is accepted.
The release decision should be made from the complete evidence package: approved documents, first-article measurements, appearance review, functional assembly, representative testing, supplier process controls, and packing trial. Keep unresolved deviations visible. Production should not begin because the sample “looks acceptable” when a critical condition has not been measured or validated.
Before closing the review, hold a short cross-functional check with design, quality, sourcing, the supplier, and the assembly owner. Confirm that each flatness tolerance requirement has an owner, a verification method, a result location, and a response when it fails. Read the drawing and inspection plan together against the actual sample. Confirm that units, sides, datums, revision identifiers, and terminology match. Record open actions separately from accepted deviations, and do not release volume production until every safety-relevant unknown has either been resolved or formally controlled by the responsible engineering authority.
Educational video
The following neutral educational video from Corning Museum of Glass explains a glass-making or material-behavior principle that supports the flatness tolerance discussion. It is background education only and does not replace the product drawing, test plan, equipment instructions, or engineering approval.
Related Kanger resources
- black ceramic glass product information
- Ceramic Glass Materials and Applications Guide
- Related dimensional specification guidance
- OEM sample-approval workflow
- Glass-ceramic packaging and shipping controls
For a drawing-led review, provide Kanger with the application, current drawing revision, material requirement, annual quantity, sample need, service conditions, and acceptance plan. The review can identify missing inputs and manufacturability questions without turning general guidance into an unsupported performance guarantee.
Frequently asked questions
Is black ceramic glass flatness tolerance a complete purchase specification?
No. It identifies the topic, but a purchase specification also needs the controlled drawing, material evidence, geometry, service conditions, assembly interfaces, inspection method, acceptance criteria, packaging, and change-control rules.
Can one approved value be used for every black ceramic glass part?
No. Size, shape, process route, support, temperature distribution, decoration, and failure consequence vary. Reuse a requirement only after confirming that the underlying conditions and validation remain applicable.
Should testing use a free panel or a complete assembly?
Use the form that answers the risk. Material coupons and free panels help isolate variables, while a production-intent assembly captures restraint, seals, frame movement, fasteners, and local heating. Many programmes need both.
What should trigger requalification?
Requalification should be considered when material source, thickness, geometry, edgework, heat process, print or coating, seal, frame, fixture, inspection method, or packaging changes in a way that could affect the approved evidence.