 Kanger Glass-ceramic Co., Ltd.
Oven door glass sealing interface design starts by defining what the seal is expected to do in the complete door: retain the panel, limit an air path, protect an edge, or provide a serviceable interface. These functions should not be assumed to belong to one gasket or adhesive. The OEM drawing must identify the glass surface, mating frame, seal path, compression or bondline control, assembly method, and oven conditions used for validation.
This drawing-led guide for oven door glass sealing interface design is written for appliance OEM, supplier-quality, and glass-engineering teams. It does not set a universal dimension, material approval, test limit, or performance guarantee. Use the released product drawing, supplier data for the exact glass and process, applicable appliance requirements, and validation on production-intent assemblies.
Define the seal function and boundary
Map the glass edge, frame, gasket, retainers, hinge side, and intended air or heat path. Distinguish a panel-retention interface from the oven’s door-to-cavity seal; they may be located on different components and perform different functions. A replacement gasket instruction does not define the glass supplier’s edge, coating, or frame-contact requirements.
Write a function statement for each interface and identify its owner. State whether the glass is mechanically captured, cushioned, bonded, or combined with a compliant seal. Where the panel is not intended to seal the oven cavity, say so to avoid loading the glass with an unplanned sealing duty.
Describe the complete geometry
Specify the seal land, edge distance, corner route, frame steps, local gaps, retainer locations, and the dimensional datums used in the assembled door. Define how the glass is centered and how corner radii align. A drawing that shows only the nominal bead or gasket size cannot establish contact around the full perimeter.
Check tolerance extremes for minimum contact and maximum compression or bondline. Include frame distortion, panel size, gasket section, installation position, and any adhesive thickness. Keep process dimensions separate from finished assembly acceptance values so the inspection plan measures the feature that controls function.
Select materials from verified service data
A gasket or adhesive should be selected using documented temperature range, compression set or cure, aging, cleaning-chemical exposure, substrate compatibility, and movement capability for the intended door position. Avoid treating a generic “high temperature” label as proof of suitability. The selected glass may be tempered, glass-ceramic, or borosilicate depending on the appliance design; compatibility must be confirmed for the actual material and surface.
Request supplier data for the exact grade, lot controls, storage life, surface preparation, and process window. Do not assume that a glass coating, print, low-emissivity layer, or surface treatment can be contacted by any sealant. Record approvals and deviations on the controlled material list.
Control glass and frame contact surfaces
Identify which glass face approaches the seal, whether printed or coated areas are permitted beneath the contact zone, and what cleanliness or preparation is required. Oil, dust, release residue, sharp frame burrs, and cleaning chemicals can affect adhesion or create local damage. Protective films must be removed at the specified assembly step.
Define handling, cleaning agent, lint control, gloves, surface inspection, and maximum hold time after preparation where these matter to the selected process. If the design uses a dry gasket, specify how contamination and displacement are detected. Keep the viewing window clear of squeeze-out and avoid fixtures that scratch or locally bend the panel.
Design corners, joints, and movement
Corners combine glass radius, frame geometry, gasket compression, splice or bead start-stop locations, and door motion. A straight-edge sample cannot represent corner compression or local squeeze-out. Define continuous paths or controlled joints and show how the seal transitions near hinges, latches, vents, or retainers.
Allow for relative movement through the expected thermal and mechanical cycle without prescribing an unsupported universal gap. Inspect for lifted gasket, loss of contact, material migration, edge pressure, and interference. Validate the assembled corner on production-intent parts and at tolerance extremes when those positions govern the outcome.
Stabilize assembly and repair process
Document gasket placement or adhesive dispensing path, bead profile if used, fixture location, compression stops, fastening sequence, cure conditions, handling limits, and rework rules. A nominal bead amount alone will not control the final interface if part location, frame distortion, or cure state varies.
Use measurable checks for presence, position, continuity, compression, bondline, or cure as appropriate to the design. Record material lot and expiry, equipment setup, operator, and inspection result. Establish whether a repaired door may return to service and which checks must be repeated after repair.
Validate sealing in the real appliance
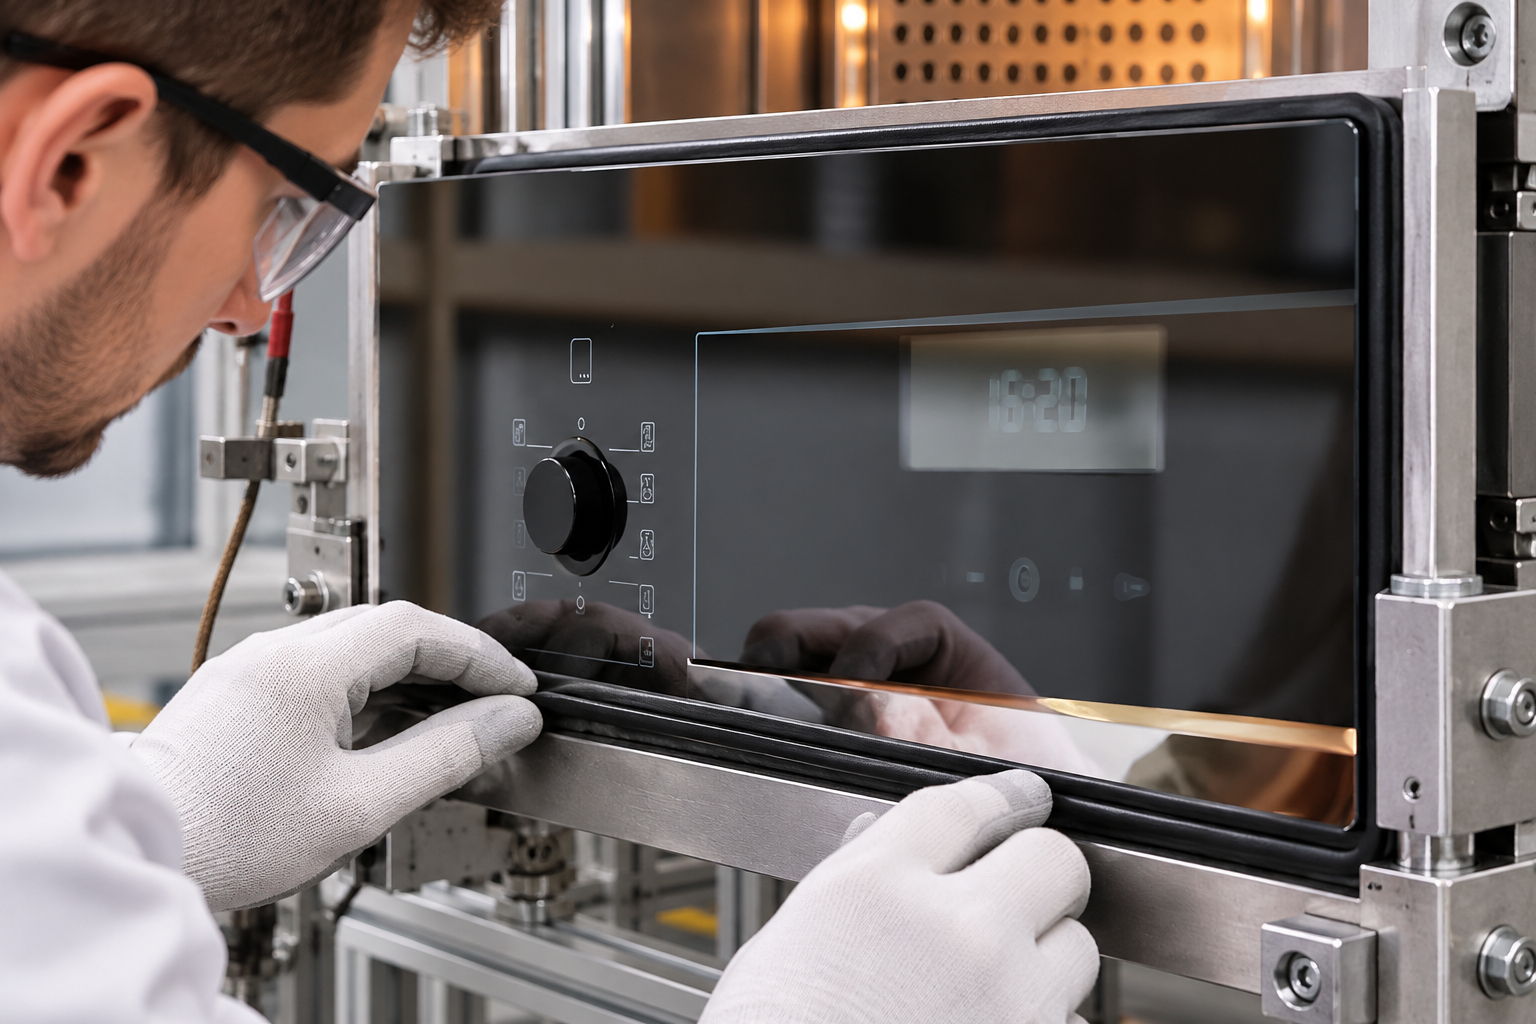
Choose tests from the actual function and risk: controlled leak or ingress checks where relevant, powered heat cycles, cooling, cleaning exposure, dwell, door operation, and aging. Define the setup orientation, fluid or tracer, exposure, sample condition, measurement locations, and acceptance before the test begins.
Evaluate both the perimeter interface and the complete appliance for unwanted heat or air path, fluid ingress, gasket migration, adhesion, glass movement, and edge damage. IEC 60335-2-6 addresses appliance-level safety for household ovens and cooking appliances; the glass and seal interface still needs product-specific engineering validation.
Set inspection and change-control rules
The released drawing, material specification, process instruction, and inspection plan should identify the seal function, approved materials, surface condition, dimensions, method, sample frequency, acceptance, and reaction plan. Keep first-article photographs and assembly records linked to the glass lot and door revision.
Review changes to pane material, thickness, coating, print, frame, gasket, adhesive, primer, fixture, cure, supplier, cleaning chemistry, or thermal profile. A seal change can alter glass movement or edge loading, so the change review should determine whether fit analysis, validation, or both must be repeated.
Engineering table
| Interface | Specify | Validation evidence |
|---|---|---|
| Seal duty | Retention, barrier, cushion, or bonded joint | Function map and ownership |
| Joint geometry | Land, gap, corner, compression or bondline | Tolerance stack and measurements |
| Surface | Glass face, print/coating allowance, cleaning | Preparation and compatibility records |
| Assembly | Placement, stops, fastening, cure or repair | First-article and process checks |
| Appliance test | Exposure tied to actual door use | Leak/ingress, cycle, and inspection results |
RFQ, first-article, and production workflow
For an RFQ, send the controlled glass drawing, appliance and door configuration, glass type or approved alternatives, glass thickness, edge and corner details, coating or print files, annual and lot quantities, packaging, and the required validation conditions. Ask the supplier to identify assumptions, proposed process limits, and deviations in writing. Keep quotation, purchase order, drawing, and inspection plan aligned to the same revision.
Before first-article approval, verify document identity, dimensions, edge quality, viewing zones, surface orientation, artwork or seal interfaces, packaging, and the topic-specific evidence in this guide. Assemble the sample with the production-intent frame, gasket, hinges, retainers, controls, and coatings when those parts influence the result. Record sample lot, equipment, setup, measured results, exposure, photographs, and disposition.
For serial production, define incoming and in-process checks with named methods, instruments, sample identity, limits, and reaction owners. Trend results by glass batch, supplier, print or seal batch, fixture, and production line. If a nonconformity appears, contain related stock, preserve original evidence before rework, compare the sample with the approved setup, and verify corrective action on a subsequent production lot.
Educational video
This neutral Corning Museum of Glass video offers background on glass coloration and surface appearance. It is educational context only and does not qualify oven-door glass or replace a product-specific test.
Related Kanger resources
- Household appliance tempered-glass product page
- Oven glass buyer guide: select by heat duty
- Oven glass-panel RFQ inspection inputs
For an application review, provide the oven-door drawing, glass position, thermal duty, coating or print files, assembly interface, and lot requirements. Kanger can review whether the RFQ package identifies the inputs needed for a drawing-based quotation.
Frequently asked questions
Should the glass perimeter gasket also seal the oven cavity?
Only if the door architecture assigns it that function and the complete assembly has been validated for it.
Is a higher-temperature adhesive automatically a better choice?
No. Compatibility, movement, cure, aging, cleaning exposure, and the actual substrate also matter.
Why inspect corners separately?
Corners combine radius mismatch, joints, compression changes, and frame movement that straight sections do not show.
What changes call for revalidation?
Changes to glass, print, coating, frame, gasket, adhesive, process, supplier, cleaning conditions, or oven duty should be reviewed.


